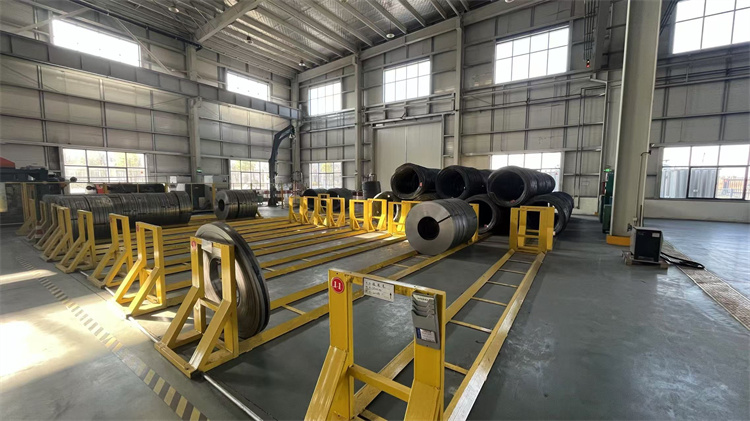
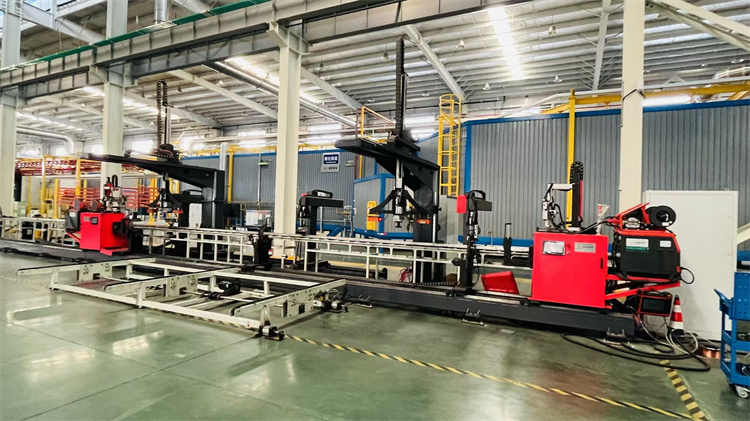
Nanjing Everack Storage Equipment Co., Ltd. was officially established in 2014, operating as a premier enterprise with over 12 years of core industry experience in industrial racking design and structural manufacturing. Situated in a modern industrial center in Nanjing, China, our manufacturing facility spans an expansive building area of 38,500 square meters. As a specialized global vendor with 9 years of dedicated export experience, our products are distributed across North America, Western Europe, and Australia, generating an impressive annual export revenue of USD 28.5 million.
Supported by a robust network of more than 1,200 upstream supply chain partners—including top-tier steel suppliers, automated powder coating providers, and precision hardware manufacturers—we serve high-tier international clients. Our primary customer base consists of third-party logistics (3PL) providers, global e-commerce distribution centers, cold storage operations, and large-scale manufacturing facilities.
Quality control is embedded at every phase of our production lines. We maintain a dedicated Quality Control department staffed by 45 certified QC inspectors. Our quality detection standard complies strictly with international metrics (ISO 9001, CE, and AS4084 structural safety guidelines).
Driven by strong engineering capabilities, Everack employs a professional team of 68 R&D engineers who utilize Finite Element Analysis (FEA) and 3D CAD modeling to engineer high-capacity, seismic-resistant storage systems. In the past year alone, our engineering unit successfully released 185 new product innovations and customized profile iterations.




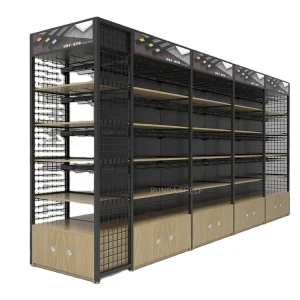
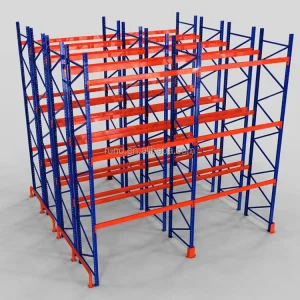
Modern global supply chains demand high-density, modular, and CE-certified storage solutions. Enterprises across North America, Europe, and Australia are increasingly transitioning toward automated warehouse systems that maximize vertical cubic storage capacity while ensuring strict compliance with local seismic and occupational safety standards.
Key procurement drivers include rapid inventory turnover in e-commerce fulfillment centers, cold storage durability requirements, and multi-tier modular adaptability for retail and wholesale environments.
As a leading CE Certified Storage Bins Factory & Exporter, we provide turnkey engineering solutions tailored to distinct industrial verticals:
Our long-term technology roadmap focuses heavily on digital transformation, IoT-enabled structural monitoring, and eco-friendly manufacturing processes. By integrating smart sensors directly into heavy-duty storage beams and vertical uprights, facility managers can monitor load stress real-time, preventing structural failures before they occur.
Furthermore, our commitment to green manufacturing involves zero-waste powder coating recycling systems, solar-powered fabrication plants, and advanced alloy metallurgy designed to reduce carbon footprints without compromising weight capacity or structural integrity.
 Everack