Explore our premium selection of industrial-grade warehouse racks, supermarket shelving units, and versatile retail display fixtures engineered for maximum space efficiency.
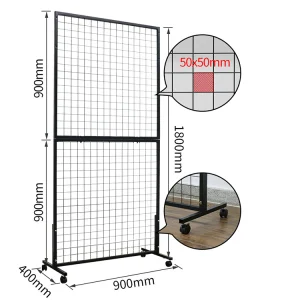
Navigating the complexities of modern supply chains through structural intelligence and advanced spatial optimization.
In the contemporary global economy, the rapid expansion of e-commerce, omni-channel retail, and automated logistics hubs has redefined the benchmarks for structural organization solutions. Enterprises across North America, Western Europe, and the Asia-Pacific region face escalating demands for warehouse density, inventory turnaround speed, and operational safety. As a leading manufacturer and exporter based in Nanjing, China, our organization solutions bridge the gap between heavy-duty industrial capability and sophisticated commercial retail merchandising.
Modern industrial ecosystems require more than standard static shelving; they demand adaptive, modular, and seismic-resistant frameworks capable of integrating with automated storage and retrieval systems (AS/RS). Our macro-level strategies focus on maximizing vertical cubic storage, reducing SKU retrieval times, and offering robust load-bearing structures that comply with international engineering standards such as ISO 9001, CE, and AS4084 guidelines.
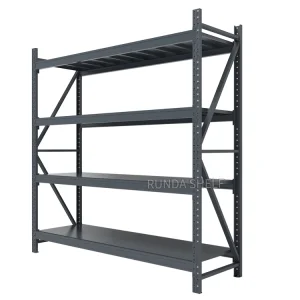
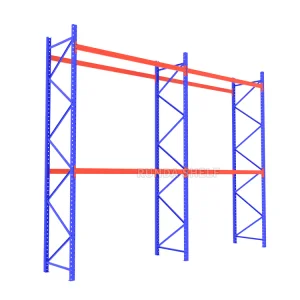
High-density selective pallet racking, multi-tier mezzanine systems, and carton flow solutions engineered for high-throughput distribution centers requiring rapid inventory processing.
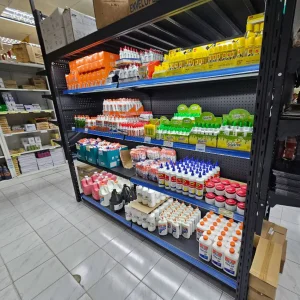
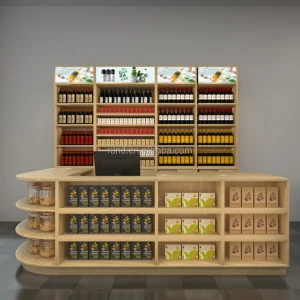
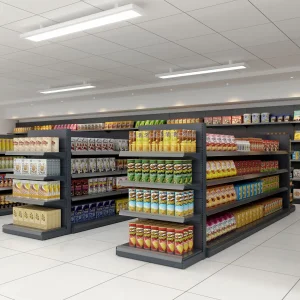
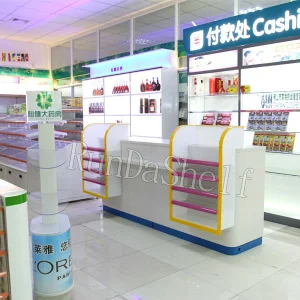
Aesthetic and versatile gondola shelving, checkout counters, and specialized display racks designed to enhance customer engagement and optimize floor space productivity.
Corrosion-resistant hot-dip galvanized finishes and specialized structural steel formulations designed to withstand sub-zero temperatures and high-humidity warehouse environments.
Combining over a decade of core industry expertise with state-of-the-art production infrastructure.
Company Overview & Background: Nanjing Everack Storage Equipment Co., Ltd. was officially established in 2014, operating as a premier enterprise with over 12 years of core industry experience in industrial racking design and structural manufacturing. Situated in a modern industrial center in Nanjing, China, our manufacturing facility spans an expansive building area of 38,500 square meters. As a specialized global vendor with 9 years of dedicated export experience, our products are distributed across North America, Western Europe, and Australia, generating an impressive annual export revenue of USD 28.5 million.
Manufacturing Strength & Supply Chain Ecosystem: Supported by a robust network of more than 1,200 upstream supply chain partners—including top-tier steel suppliers, automated powder coating providers, and precision hardware manufacturers—we serve high-tier international clients. Our primary customer base consists of third-party logistics (3PL) providers, global e-commerce distribution centers, cold storage operations, and large-scale manufacturing facilities.
Uncompromising safety protocols backed by certified quality control inspectors and advanced testing methodologies.
Quality Assurance & Inspection Standards: Quality control is embedded at every phase of our production lines. We maintain a dedicated Quality Control department staffed by 45 certified QC inspectors. Our quality detection standard complies strictly with international metrics (ISO 9001, CE, and AS4084 structural safety guidelines).
Product Inspection Methods:
We ensure that every organization solution exported to global markets meets or exceeds regional building codes and safety regulations. From seismic loading requirements in earthquake-prone zones to stringent fire safety clearances, our engineering team provides complete compliance documentation, calculation sheets, and third-party verification reports upon request.
Understanding that operational environments vary drastically between regions, we provide tailored application support. Whether designing for high-density urban retail stores in Western Europe or sprawling distribution hubs in North America, our technical consultants work closely with local contractors to ensure seamless integration, rapid on-site assembly, and long-term durability.
Leveraging advanced Finite Element Analysis (FEA) and 3D CAD modeling to engineer high-capacity storage systems.
R&D Engineering & Customization Capability: Driven by strong engineering capabilities, Everack employs a professional team of 68 R&D engineers who utilize Finite Element Analysis (FEA) and 3D CAD modeling to engineer high-capacity, seismic-resistant storage systems. In the past year alone, our engineering unit successfully released 185 new product innovations and customized profile iterations.
Customization Options:
A visual tour of our precision manufacturing lines, automated rolling mills, and robotic welding stations.
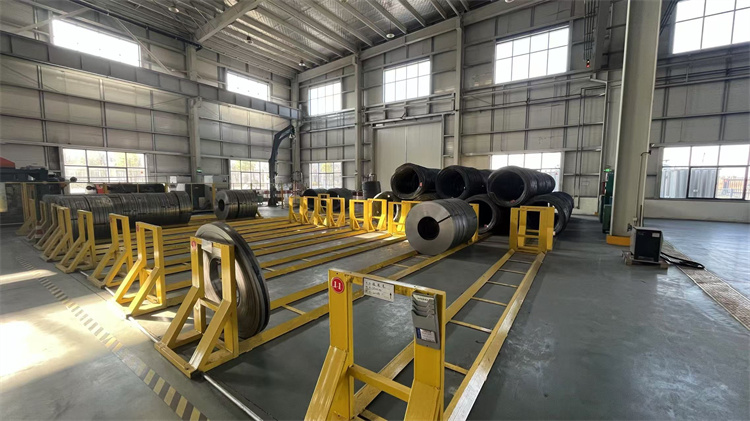


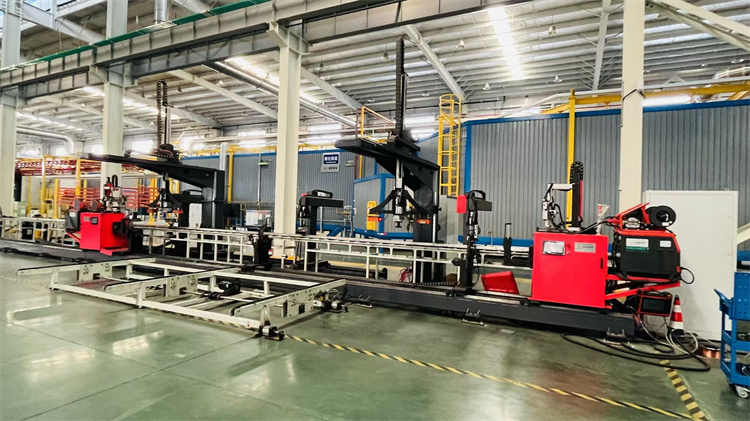


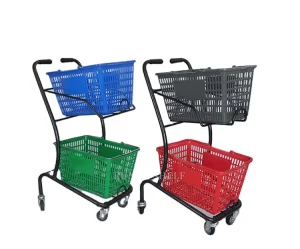
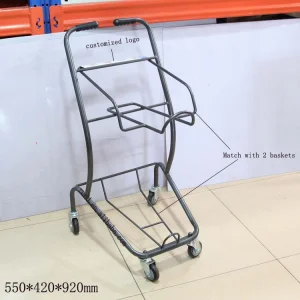
Discover our comprehensive range of shopping carts, combination display racks, grocery shelving, and heavy-duty industrial pallet systems.
Pioneering the next generation of smart warehousing and automated organization systems.
Developing IoT-enabled smart racks equipped with automated weight sensors, RFID inventory tracking, and seamless compatibility with Autonomous Mobile Robots (AMRs) for lights-out fulfillment centers.
Transitioning toward closed-loop steel recycling, zero-VOC powder coating formulations, and energy-efficient laser cutting machinery to minimize environmental impact across our supply chain.
Engineering plug-and-play modular storage frameworks that allow businesses to effortlessly reconfigure warehouse layouts and retail floors in response to shifting consumer demands.
Expert answers regarding our organization solutions, manufacturing capabilities, and global export services.
 Everack