Engineered for maximal spatial efficiency, structural safety standard compliance, and heavy load capacity across worldwide logistics network operations.
Analyzing macro-economic shifts, automated intralogistics demand, and the pivotal role of Chinese steel manufacturing in modern supply chain infrastructure.
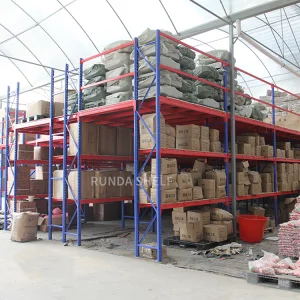
The global industrial storage racking sector is undergoing an unprecedented structural revolution. Driven by cross-border e-commerce expansion, third-party logistics (3PL) optimization, and hyper-localized fulfillment hubs, the demand for high-density, multi-tier racking systems is projected to exceed USD 16.8 Billion by 2030. Enterprise operations require structural steel frameworks capable of bearing dynamic live loads, resisting seismic activity, and integrating seamlessly with Automated Storage and Retrieval Systems (ASRS).
Modern distribution centers no longer view storage racks as passive metal frames, but as essential structural assets that directly determine throughput velocity, vertical space utilization ratios, and operational safety metrics.
China has consolidated its leadership as the world's premier production and export nexus for industrial racking and retail display systems. China's competitive supremacy rests upon three core pillars: integrated raw material procurement (high-yield cold-rolled steel coils Q235B/Q355B), fully automated cold-roll forming lines, and rigorous international quality certification protocols (AS4084, ISO 9001, CE, and FEM 10.2.02).
As an industry pioneer, China's racking engineering ecosystem combines cost efficiency with extreme structural customization—allowing global enterprise buyers in North America, Western Europe, and Australia to deploy structural steel mezzanine and pallet rack systems tailored to precise architectural footprints.
Nanjing Everack Storage Equipment Co., Ltd. delivers industrial-grade racking architecture backed by over a decade of precision structural engineering and worldwide export authority.
Nanjing Everack Storage Equipment Co., Ltd. was officially established in 2014, operating as a premier enterprise with over 12 years of core industry experience in industrial racking design and structural manufacturing. Situated in a modern industrial center in Nanjing, China, our manufacturing facility spans an expansive building area of 38,500 square meters. As a specialized global vendor with 9 years of dedicated export experience, our products are distributed across North America, Western Europe, and Australia, generating an impressive annual export revenue of USD 28.5 million.
Supported by a robust network of more than 1,200 upstream supply chain partners—including top-tier steel suppliers, automated powder coating providers, and precision hardware manufacturers—we serve high-tier international clients. Our primary customer base consists of third-party logistics (3PL) providers, global e-commerce distribution centers, cold storage operations, and large-scale manufacturing facilities.
Precision computational modeling ensures seismic stability, optimal steel mass distribution, and tailored structural load ratings.
Driven by strong engineering capabilities, Everack employs a professional team of 68 R&D engineers who utilize Finite Element Analysis (FEA) and 3D CAD modeling to engineer high-capacity, seismic-resistant storage systems. In the past year alone, our engineering unit successfully released 185 new product innovations and customized profile iterations.
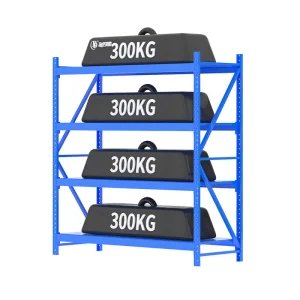
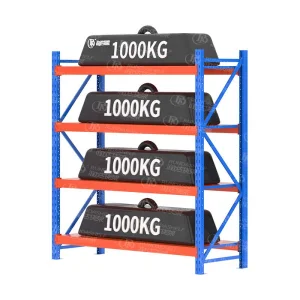
Custom beam span, upright profile thickness, and structural load capacity (from 500 kg to 4,000 kg per level). We tailor profile geometries to achieve maximal moment of inertia while eliminating unnecessary material dead weight.
Tailored color finishes, electrostatic epoxy powder coating, or hot-dip galvanizing for outdoor and cold-room environment resistance. Engineered with modular vertical spacing, seismic bracing designs, and bespoke safety accessory integrations.
Strict structural safety testing and material verification complying with ISO 9001, CE, and AS4084 guidelines.
Quality control is embedded at every phase of our production lines. We maintain a dedicated Quality Control department staffed by 45 certified QC inspectors. Our quality detection standard complies strictly with international metrics (ISO 9001, CE, and AS4084 structural safety guidelines).
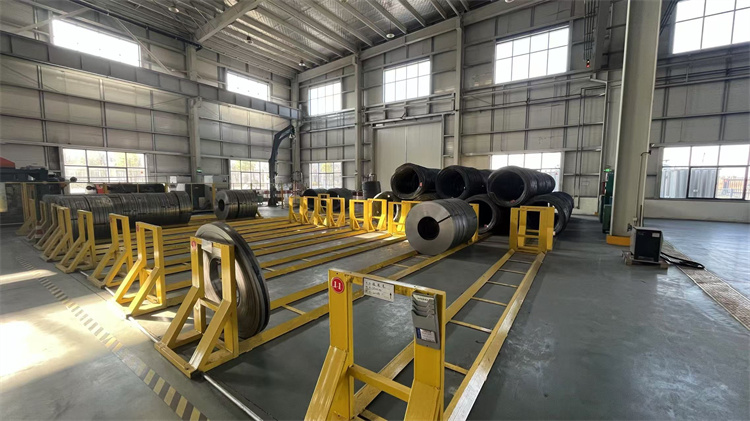
Explore our complete end-to-end automated manufacturing workflow—from raw steel coil processing to CNC roll forming, robotic welding, and powder coating.
Raw Materials

Wiredrawing

Strengthening

Strengthening Rib

Metal Mesh Production

Steel Coil Material

Precision Cutting

Profile Bending

Automatic Punching

P-Beam Rolling

Diagonal Brace Rolling

Occluding Beam Rolling

Column Production

Automatic Welding

Powder Spraying

Plate Shearing Machine

Plate Bending Machine

Sawing Machine

Punching Machine

Laser Cutting Machine
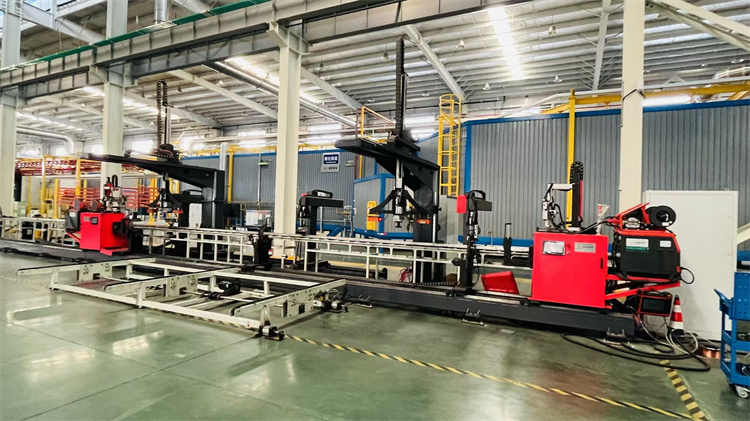
Automatic Welding Unit

Grinding Machine

Shot Blasting Machine

Spraying Production Line

Hot Cleaning Furnace

CNC Curve Gear Grinding

Milling Machine

Wiredrawing Machine

Strengthening Machine

Strengthening Rib Machine

Metal Mesh Line

P-Beam Rolling Mill

Diagonal Brace Mill

Occluding Beam Mill

Column Production Line

Welding Robot Unit
From sub-zero cold chain logistics to high-throughput retail operations, explore how custom racking profile geometries maximize operational profitability.
Cold storage warehouses face extreme thermal stress and moisture condensation. Everack engineers structural drive-in and shuttle racking systems using hot-dip galvanized steel coatings and high-impact structural alloys. This prevents hydrogen embrittlement and surface degradation at temperatures down to -30°C while achieving high spatial density.
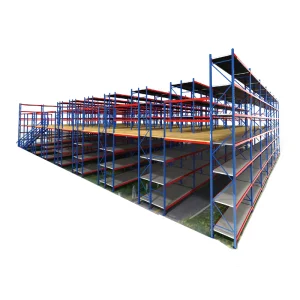
To optimize high-value warehouse footprint, multi-tier mezzanine racks double or triple vertical floor space. Integrated with modular staircases, conveyor chutes, and safety handrails, our custom mezzanine frameworks support intense piece-picking operations for global e-commerce distribution centers.
Handling long, bulky items like steel pipes, timber, and aluminum extrusions requires specialized dynamic loading systems. Our automated roll-out cantilever racking features crank-out arms allowing overhead cranes to pick materials seamlessly, reducing handling damage and floor congestion.
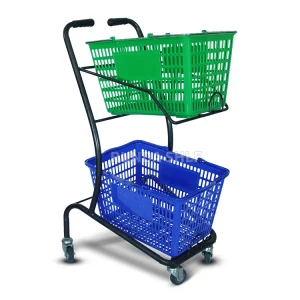
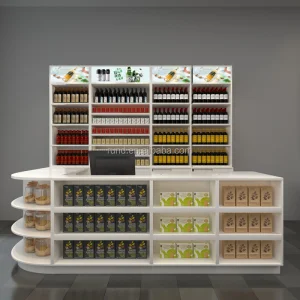
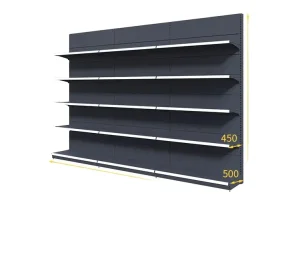
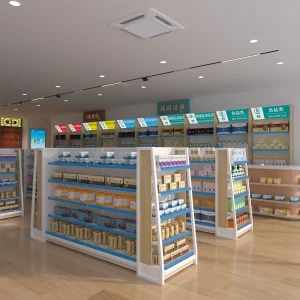
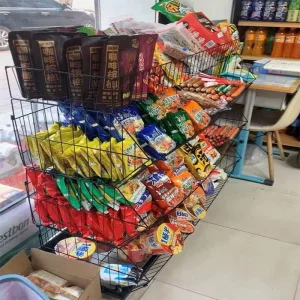
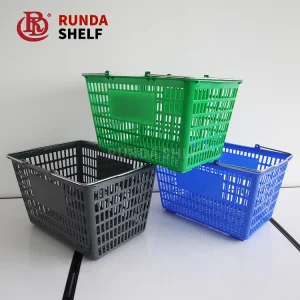
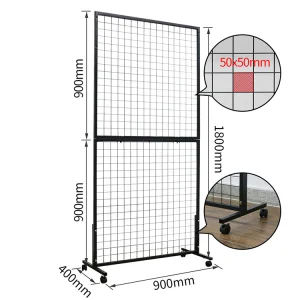
Retail visual merchandising demands structural durability combined with modular aesthetics. Our range of single/double-sided gondola display shelves, snack display racks, wire baskets, and cashier desks deliver flexible customer flow control, high aesthetic presentation, and long service lifespan.
Pioneering the transition from static physical structural racks to IoT-integrated, AI-monitored smart warehouse environments.
Integration of strain-gauge sensors directly into critical upright columns and load beams. Real-time telemetry alerts facility managers to structural overload conditions, forklift impact deformations, or unexpected seismic shear stress.
Designing standardized micro-tolerance guide rails and laser-reflective profiles optimized for Autonomous Mobile Robots (AMR) and four-way radio shuttle cars, accelerating automated pick-pack cycles.
Transitioning manufacturing processes to 100% recycled high-yield steel stock and VOC-free electrostatic powder coatings, reducing carbon footprint while fulfilling international ESG supply chain compliance.
Expert answers addressing critical structural engineering considerations, standard compliance, custom fabrication, and international freight logistics.
Our heavy-duty pallet racking, mezzanine frameworks, and cantilever systems are designed and tested strictly in compliance with international structural standards: AS4084-2012 (Australian Steel Storage Racking Standard), FEM 10.2.02 (European Racking Federation Standard), and ANSI/RMI MH16.1 (American National Standard for Industrial Steel Storage Racks). We hold ISO 9001 and CE quality certifications.
Our R&D team uses advanced Finite Element Analysis (FEA) software to model structural behavior under uniform distributed loads (UDL), dynamic forklift impacts, and localized point forces. Every load calculation considers beam span deflection limits (L/200), column buckling resistance, and seismic zone requirements before prototype physical stress testing.
For standard indoor warehouse environments, we utilize heavy-duty electrostatic epoxy-polyester powder coating (60-80 micron thickness). For coastal regions, cold storage facilities, or outdoor deployment, we offer Hot-Dip Galvanizing (HDG) according to ISO 1461 standards, delivering 50+ years of maintenance-free rust resistance.
Standard custom production lead time is 15 to 25 business days from engineering drawing sign-off. Backed by our 38,500 m² factory footprint and 1,200+ upstream material suppliers, we can process high-volume structural orders (e.g., 20 to 50 40ft HQ containers) efficiently with synchronized batch deliveries.
Explore our specialized retail display units, automated cantilever systems, and heavy-duty store storage solutions.
 Everack